

Scope
Products, processes, dates and locations examined.
Walk the proposed order from material receipt to dispatch and mark where ownership changes. A useful audit records what the site controls, what a partner performs, and which evidence reconnects every handoff.
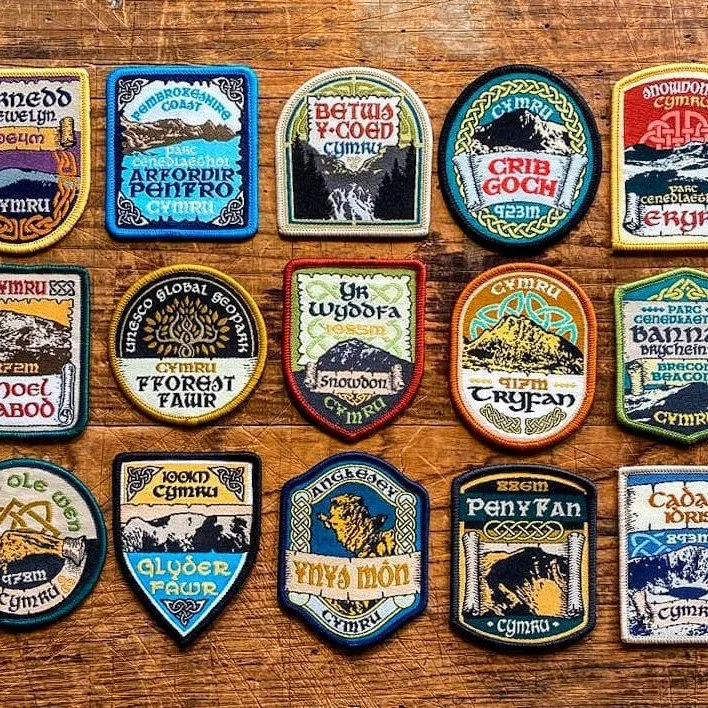
A factory visit becomes vague when the team asks whether a site can make “patches” in general. State the target product, artwork status, materials under consideration, dimensions, attachment direction, volume, packing destination and planned production window. Record the legal entity, physical address, areas visited, people interviewed and documents sampled. The primary query wholesale patch makers can describe many commercial roles; the charter should distinguish factory, trading office, development studio and external specialist. Note excluded areas and unavailable records so the report does not imply complete coverage.
Products, processes, dates and locations examined.
Buyer, technical, quality and factory participants.
Selected work orders, lots, operators and records.
Information not observed or independently verified.
Catalog variety is a starting point, not proof that every operation occurs under one roof. In the Product 8 row, TB-EF3334FD9DC1 identifies a custom-size patch made with high-quality embroidery thread; its listed minimum is 100 pieces. Product 35 records TPU, 7.5 cm, MOQ 100 and code DG-ZK-001. Product 50 records silicone, 6 by 8 cm, MOQ 100 and code GZ-FC-009. The audit must verify the proposed route for each chosen construction rather than using one product photo to certify another process.
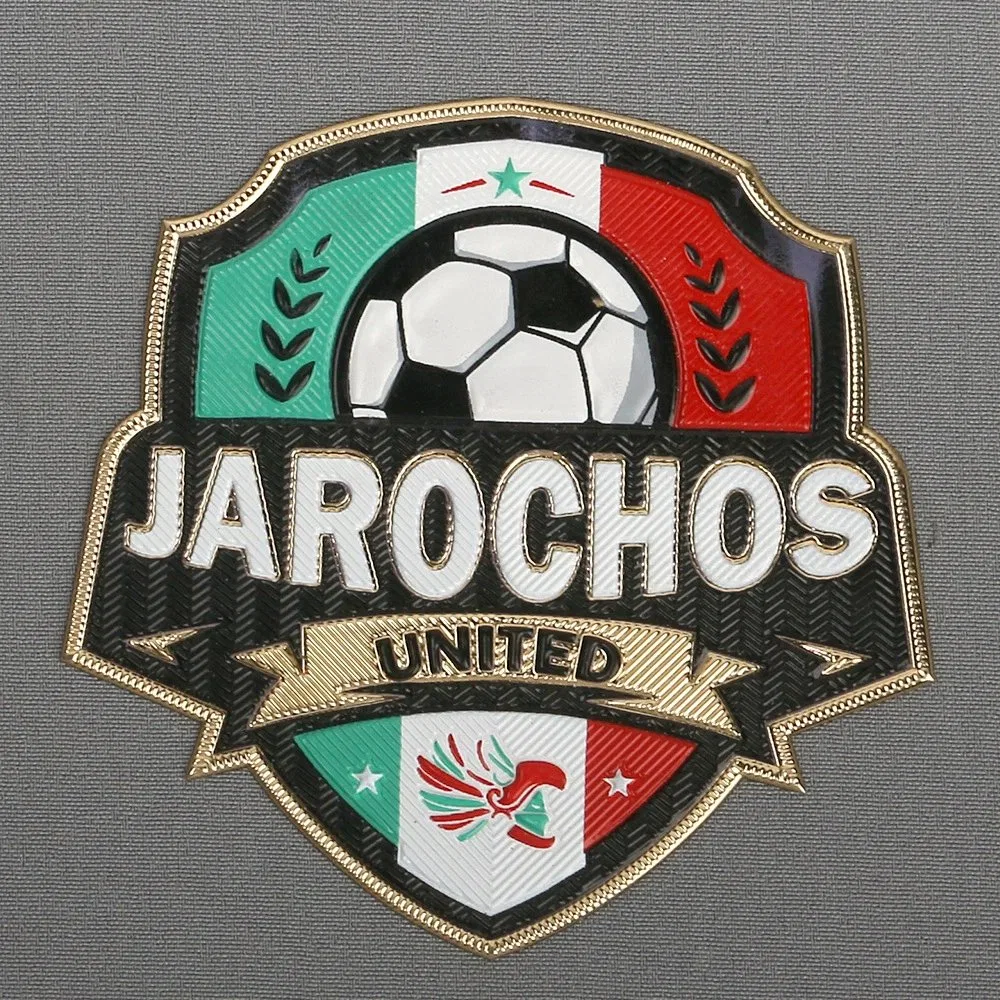
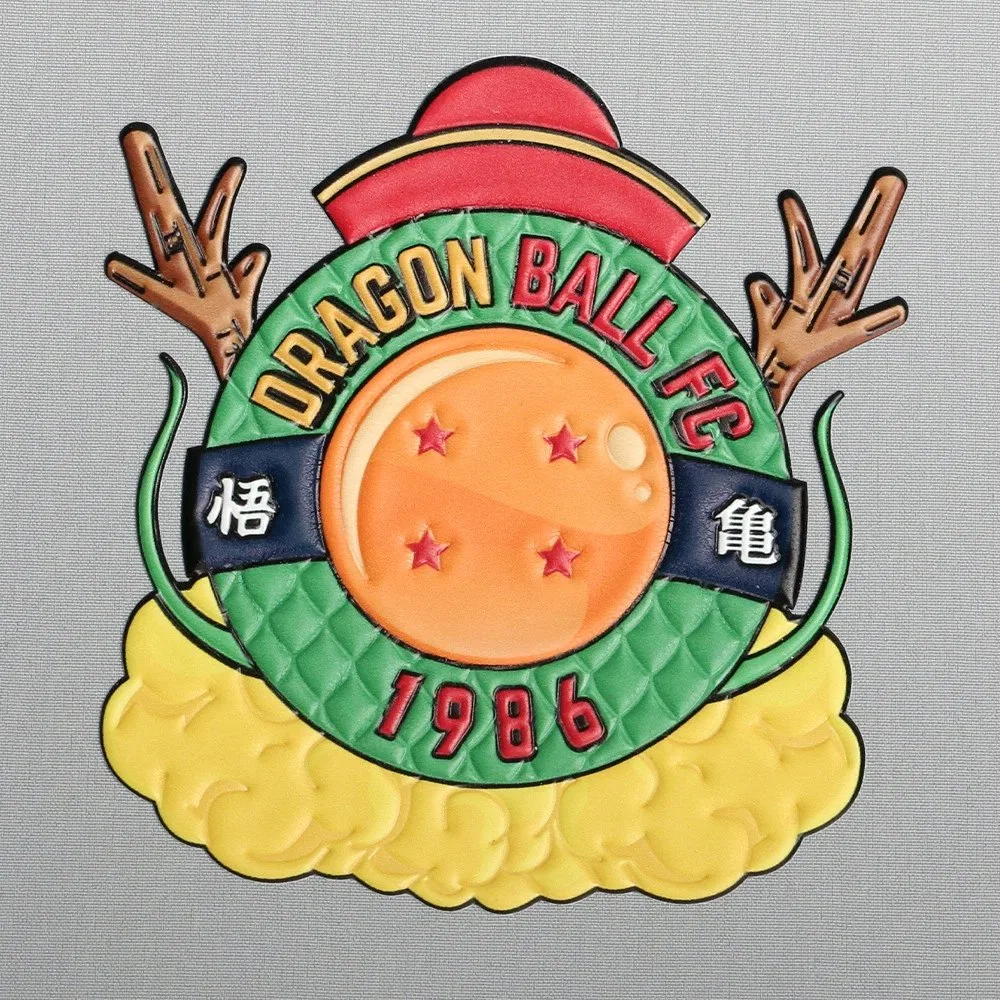
Choose a recent or representative order close to the intended construction and follow its identifiers. Begin at material receiving, then visit artwork preparation, production, in-process inspection, finishing, final acceptance, packing and dispatch. At each stop, ask an operator to explain which document authorizes the work and how status is marked. Compare the explanation with the record rather than accepting a presentation slide. If materials leave the building, capture dispatch identity, external processor, return acceptance and quarantine controls. This route reveals whether wholesale patches makers operate a connected system or a collection of informal handoffs.
The private-label factory audit offers a broader accessory framework; this page narrows the walk to patch-specific ownership and records.
Equipment lists should name the process, capacity range, maintenance status, operator qualification and product limitations relevant to the request. Observe asset identification and a current maintenance or verification record where appropriate. Do not infer capability from an idle machine whose tools, software or trained operator are unavailable. For bespoke iron on patches bulk, separate patch formation from reverse application and garment testing; those may have different owners. For raised logo work, ask how mold or tooling approval is controlled. The raised-logo material guide helps frame TPU and silicone questions without claiming identical production routes.
| Operation | Evidence | Boundary |
|---|---|---|
| Artwork preparation | Software, revision input, approval output | Who releases the production file? |
| Patch formation | Asset, operator, work instruction | Which steps leave the site? |
| Reverse or transfer | Quoted construction and test record | Which receiving material was used? |
Ask how ordered materials are specified, approved, received, labeled, stored and issued. Select a thread, textile base, TPU or silicone input associated with the sampled order and follow its identity into work in process. Observe how rejected or expired material is separated under the site's actual procedure without assuming a universal shelf rule. Compare supplier documentation with internal receiving results. A garment accessories manufacturer may manage many similar colors and compounds, so visual resemblance is not enough; the system needs a reliable way to prevent substitution and to record an authorized change.
Approved material identity and current revision.
Quantity, condition and acceptance status.
Lot or batch connection to the work order.
Physical hold and documented disposition.
Select a completed inspection and ask a second person to explain how the result was reached. The record should identify the product, revision, lot, sample basis, characteristic, method, tool when used, result, inspector and disposition. Observe how dimensions are defined so two inspectors measure the same boundary. Review the status and identification of measurement tools appropriate to the site. Visual criteria need approved references or defect descriptions rather than memory. Use the quality-control checklist as a question source, but replace transfer-specific attributes with those belonging to the audited patch.
| Audit test | Pass evidence | Concern |
|---|---|---|
| Repeat measurement | Declared method returns a comparable result | Boundary changes by inspector |
| Visual call | Finding links to an approved reference | Acceptance depends on recollection |
| Disposition | Affected quantity and authority are recorded | Rejected units return to stock |
Choose one packed carton and trace it backward to final inspection, work order, material identities and approved artwork. Then choose one input lot and trace forward to affected work, remaining stock and dispatch destinations. Record how long the exercise takes and where human memory fills gaps. If an external processor appears, include outgoing count, returned count, loss or scrap treatment and acceptance result. Review how customer property and confidential artwork are controlled. Traceability depth should match the order's risk and contract; the audit report must state what was demonstrated instead of declaring absolute end-to-end coverage.
Classify findings by the buyer's documented method and distinguish immediate containment from corrective action. A missing label may require the affected stock to be held now, while the root cause and prevention plan take longer. Assign owners and due dates, request objective completion evidence and schedule an effectiveness check proportionate to risk. Record whether sourcing approval is open, conditional or declined. Do not convert an unverified photograph into closure. The final report should preserve strengths as well as gaps, identify sampled records, declare limitations and show which decisions remain with the buyer.
Include statement, evidence, affected scope, containment, cause method, action, owner, due date, verification and sourcing consequence. Link the card to the product and factory location covered by the audit.
These answers separate what the audit sampled from what the factory may be asked to confirm later.
The audit tests whether the process, people, records and external handoffs described for a proposed order are visible and controlled. It is not a certificate and cannot replace the buyer’s own due diligence.
No. Record which step is external, why it is used, who qualifies the provider, how materials travel and which organization accepts the returned work.
No. Products 8, 35 and 50 demonstrate different catalog directions. The audited site must still show order-specific ownership and evidence for embroidery, TPU or silicone work it proposes.
Look for purchase identity, receiving status, batch or lot references, work-order linkage, inspection results, nonconformance disposition and final carton identity appropriate to the facility’s system.
Assign each finding an owner, containment action, root-cause method, corrective action, evidence due date and effectiveness review. Keep open items visible in sourcing approval conditions.